Background
The client operated a 110 m³ timber drying kiln powered by a coal-fired hot air furnace. High energy consumption, poor temperature and humidity control, and inconsistent final moisture content across the board were the main bottlenecks holding back timber quality and operating margins.
Retrofit solution
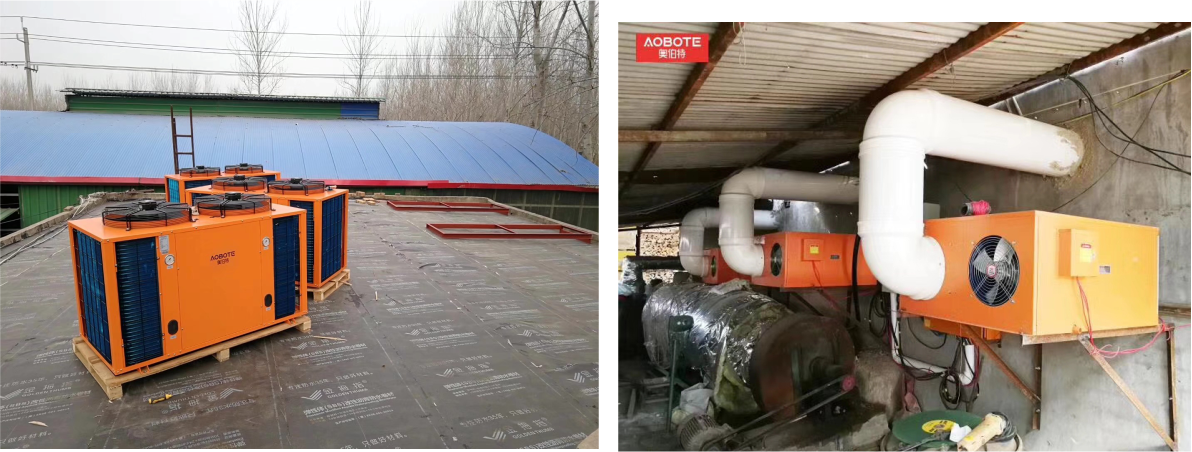
We replaced the coal-fired furnace with AOBOTE heat pump dehumidification drying units matched to the 110 m³ kiln volume. The closed-loop system recycles heat and continuously removes moisture, keeping the chamber at a stable low temperature while air circulation is maintained evenly through the stack.
Results
After commissioning, the moisture content of the dried panels became uniform across every load. Energy consumption was reduced by over 60% compared to the previous coal-fired operation, and the kiln now runs with automatic, repeatable drying curves instead of manual furnace control.